Supporting the Future of Automotive Testing in the USA

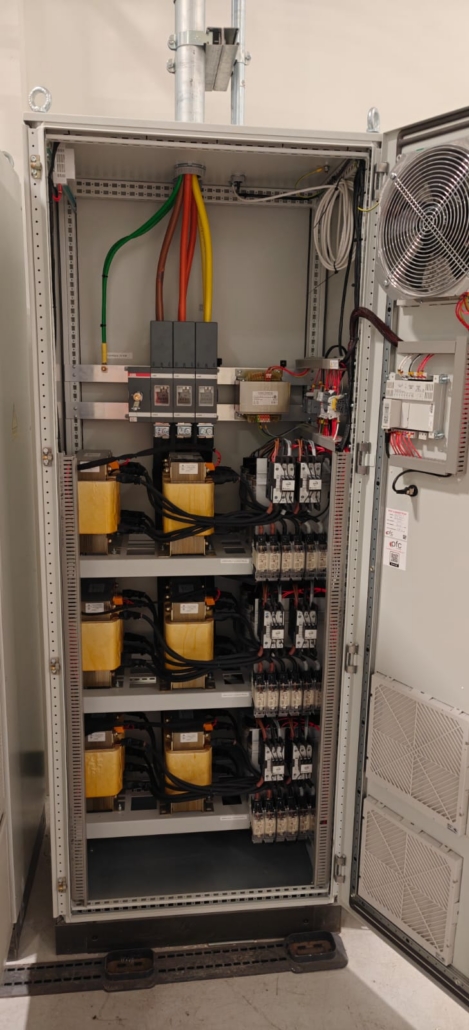
The PFC Engineering team recently travelled from the UK to Los Angeles, USA, to commission a bespoke 350 kVAr Power Factor Correction (PFC) system and 330A Active Harmonic Filter (AHF) at a major global automotive manufacturer’s testing facility.

Both systems were custom-designed and manufactured by PFC Engineering in the UK, specifically to meet US electrical requirements and the customer’s individual design requirements.

Designed, Built and Tested in the UK

Before making the journey across the Atlantic, both systems were fully assembled and tested at PFC Engineering’s UK facility.

Building and testing the equipment in the UK allowed the engineering team to verify the systems, control equipment and protection arrangements before they left for the USA. This provided an opportunity to identify and resolve any issues before the equipment reached site, helping to make the final installation and commissioning process as efficient as possible.

Once the factory testing was complete, the equipment was carefully prepared and shipped from the UK to Los Angeles, ready for installation and final commissioning at the customer’s facility.

This approach meant that when the PFC Engineering engineers arrived on site, the equipment had already been built, checked and tested, allowing the team to concentrate on installation checks, site-specific settings and final commissioning.

350 kVAr Power Factor Correction System

The PFC system has been designed to provide reliable and automatic power factor correction as the facility’s electrical demand changes.

The system consists of:

  • 6 × 54 kVAr PFC stages
  • 690V-rated capacitors
  • Lovato DCRL8 digital power factor controller

The staged design allows the system to automatically adjust the amount of correction in operation, bringing capacitor stages in and out of circuit as required by the site load.

This provides efficient power factor correction without unnecessarily overcompensating the electrical system.

330A Active Harmonic Filter

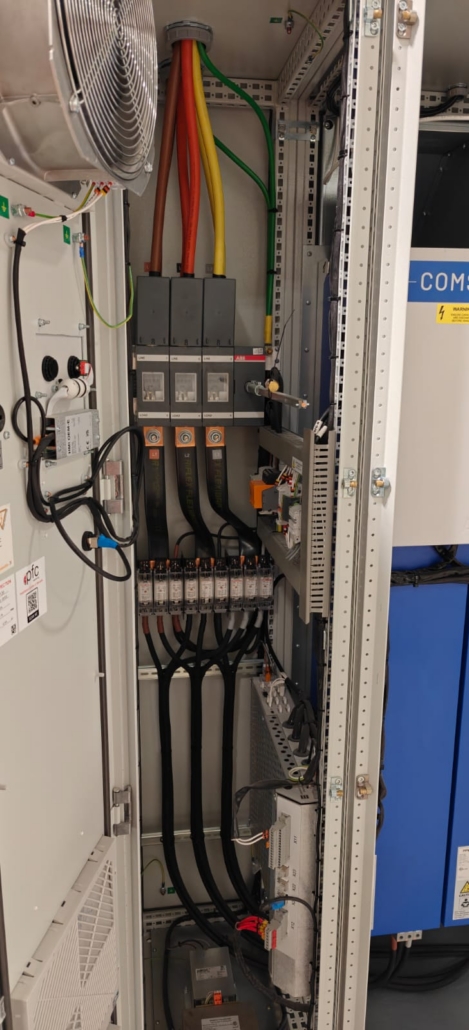
Alongside the PFC system, PFC Engineering commissioned a 330A Active Harmonic Filter, consisting of:

  • 3 × 110A Comsys filter modules
  • IEEE 519 AutoTune functionality
  • Automatic operation in response to changing site conditions

The AHF is designed to respond dynamically to the harmonic currents generated by the facility’s equipment. Using the IEEE 519 AutoTune function, the system can optimise its operation to provide effective harmonic mitigation as the electrical load changes.

The unit is configured to automatically come in and out of circuit depending on the site load, providing harmonic correction when it is required.

Immediate Improvements Following Commissioning

The commissioning produced some very positive results.

Following the AHF being brought into operation, the site reported that the flickering LED lighting was no longer occurring.

The facility’s EV chargers were also able to continue operating correctly. Prior to commissioning, the chargers had been experiencing faults when the active harmonic filter was not running.

This demonstrated the importance of managing power quality within modern electrical installations, particularly at facilities incorporating high-power electronic equipment such as EV charging infrastructure, testing equipment and other power electronic loads.

Two Days on Site in Los Angeles

PFC Engineering engineers spent two days on site completing the final commissioning, testing and optimisation of both systems.

With the installation successfully commissioned and operating as intended, the team were able to grab a little downtime before heading back to the UK — including some well-earned time around Manhattan Beach.

It was a great opportunity to combine PFC Engineering’s UK-based power quality expertise with a challenging international installation, delivering a bespoke solution designed specifically around the customer’s requirements.

Another Successful International Commissioning

The project highlights PFC Engineering’s ability to design, manufacture, factory-test, ship and commission bespoke PFC and active harmonic filtering systems internationally.

From the initial design and manufacture in the UK, through factory testing and international shipping, to final commissioning in Los Angeles, the project was delivered as a complete power quality solution tailored specifically to the customer’s requirements.
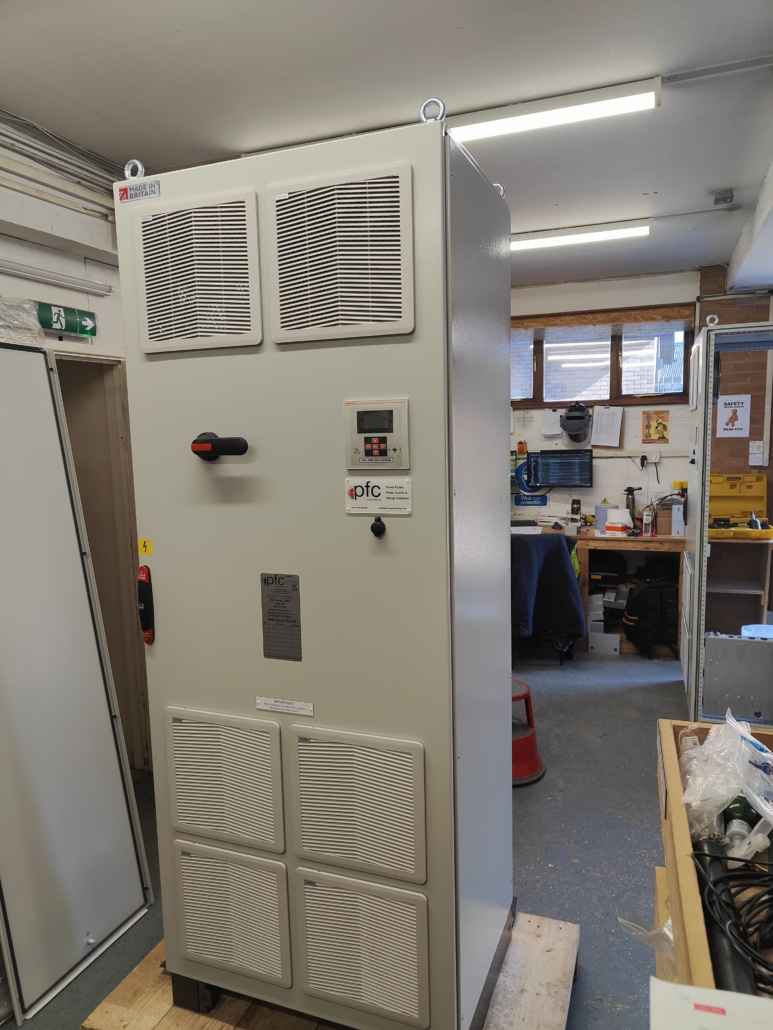
 

Power quality issues are becoming increasingly common in modern commercial and industrial installations, particularly in dense urban environments where harmonic distortion can significantly impact electrical performance. We were recently tasked with rebuilding a power factor correction (PFC) system at a site in Central London, addressing both component failure and rising harmonic levels.

The Challenge

The existing PFC unit had suffered multiple failures, with all three 50kVAr stages no longer operational. In addition, the site was experiencing a voltage total harmonic distortion (VTHD) level of 4% and rising, indicating increasing harmonic stress on the system.

Attempting to restore the system using standard capacitor banks alone would have risked amplifying harmonic issues further—a common problem in installations with non-linear loads.

The key objectives were:

  • Restore reliable power factor correction
  • Prevent further harmonic amplification
  • Improve overall system stability and performance

The Solution

To address both the failed equipment and the harmonic concerns, we carried out a full rebuild of the PFC system incorporating detuning reactors.

Key Elements of the Upgrade:

  • Detuning Reactors Installed
    These were integrated to prevent resonance and suppress the impact of harmonics, ensuring the new system would not contribute to rising distortion levels.
  • Reconfigured Capacitor Stages
    Two new PN54 capacitor trays were installed, split into 25kVAr and 50kVAr stages. This provided more flexible step control and improved responsiveness to varying load conditions.
  • Lovato DCRL8 Controller
    A new, advanced controller was fitted to provide accurate power factor regulation and improved monitoring of system performance.
  • New Control Wiring & Power Cabling
    All associated wiring was upgraded as part of the rebuild, ensuring long-term reliability and compliance with current standards.

Installation & Commissioning

The project was completed by a two-engineer team in just one day, with careful planning ensuring no disruption to site operations.

Following installation and commissioning, the system delivered immediate results:

  • Power factor improved from 0.9 to unity (1.0)
  • No increase in harmonic distortion levels, despite restoring full PFC functionality

This demonstrated the effectiveness of the detuned design in maintaining power quality while achieving optimal correction.

Environmental Responsibility

All redundant equipment was removed from site and disposed of responsibly, in line with current environmental and waste management regulations.

The Outcome

The upgraded system now provides:

  • Stable, reliable power factor correction
  • Protection against harmonic-related issues
  • Improved efficiency without compromising power quality
  • Greater flexibility in load management

Conclusion

As harmonic distortion becomes more prevalent in modern electrical systems, integrating detuning reactors into PFC installations is no longer optional—it’s essential. This project highlights how the right design approach can resolve existing issues while future-proofing the installation.


Maintaining efficient electrical systems is critical in high-demand industrial environments, especially in sectors like grain processing where large motors and continuous operations place significant load on power infrastructure. Recently, we completed a full replacement of a power factor correction (PFC) unit at a major UK grain processing plant, upgrading both reliability and performance in a single-day installation.

The Challenge

The existing PFC unit had reached the end of its service life. It had become unreliable and was based on outdated technology, resulting in reduced efficiency and increased risk of failure. The site was operating at a lagging power factor of approximately 0.89, leading to unnecessary reactive power demand and potential financial penalties from the utility supplier.

Given the plant’s operational demands, maintaining power quality and improving efficiency were essential priorities.

The objective was clear:

  • Replace the failed unit quickly to minimise disruption
  • Upgrade to modern, more reliable components
  • Improve overall system performance and safety

The Solution

We installed a new custom built power factor correction unit in the same location as the original, utilising the existing cabling infrastructure. This approach significantly reduced installation time and complexity while keeping costs under control.

Key Upgrades Included:

  • 480V Rated Capacitors
    The new capacitors provide improved durability and performance, better suited to modern industrial electrical systems and fluctuations in load.
  • Soft Switching Contactors
    These reduce electrical stress during switching operations, extending the lifespan of components and improving overall system reliability.
  • Lovato DCRL5 Power Factor Controller
    A modern controller offering precise regulation, improved monitoring, and enhanced control over the correction process to maintain optimal efficiency.
  • Additional Fire Trace Protection
    At the client’s request, we integrated a fire trace protection system within the unit. This adds an important layer of safety, helping to protect internal components and mitigate fire risk—particularly important in environments where dust and combustible materials may be present.

Installation & Commissioning

The entire project was completed efficiently by a two-engineer team in just one day. Careful planning and the reuse of existing infrastructure allowed for a streamlined installation process with minimal disruption to site operations.

Once installed, the system was fully commissioned, tested, and brought online. The results were immediate and measurable, with the site’s power factor improving from 0.89 lagging to unity (1.0). This correction significantly reduced reactive power draw and optimised the overall electrical efficiency of the plant.

Environmental Responsibility

All old equipment was removed from site and disposed of responsibly in line with current environmental regulations, ensuring full compliance while minimising environmental impact.

The Outcome

The plant now benefits from:

  • Power factor improvement from 0.89 to unity, reducing reactive power charges
  • Improved electrical efficiency across the installation
  • Increased reliability and reduced maintenance requirements
  • Enhanced safety due to upgraded protection systems

Conclusion

Upgrading aging power factor correction equipment is a smart investment for any industrial facility. Not only does it improve efficiency and reduce operational costs, but it also ensures compliance with modern standards and enhances overall site safety.

This project demonstrates how, with the right approach and expertise, even critical electrical upgrades can be completed quickly, safely, and with minimal disruption—while delivering immediate, measurable performance improvements.


Power Factor Correction Upgrade at Magistrates Court – South of England

At PFC Engineering, we’re often called in to assess and resolve issues where existing power factor correction (PFC) systems are no longer suitable for the demands of a site. This was recently the case during a scheduled maintenance inspection at a magistrates court in the south of England.

Initial Findings

During our inspection, it quickly became clear that the existing PFC system was not fit for purpose. The installation consisted of a fixed 50kVAr unit, which was insufficiently flexible for the site’s varying load profile.

In addition to this, a more serious issue was identified upstream — the PFC unit was being supplied via a fuse switch that had begun to fail, with visible signs of overheating and burning on the L3 phase. This posed a significant reliability and safety risk, requiring urgent attention.

Load Survey & System Assessment

As part of our standard process, we carried out a load survey while on site to better understand the electrical characteristics of the installation. The results showed that:

  • The overall kVAr demand of the site was adequate
  • However, the existing correction stage was too large and inflexible
  • The fixed nature of the system meant it could not adapt to changing load conditions

This was particularly problematic during periods of low demand, such as overnight and weekends. With the capacitor permanently in circuit, the site was being pushed into a leading power factor, which can be just as undesirable as a lagging one—potentially leading to voltage instability and increased stress on electrical equipment.

Proposed Solution

To resolve both the safety issue and improve overall performance, we recommended a full upgrade of the PFC system.

Key elements of the solution included:

  • Removal of the failing fuse switch
  • Installation of a new FS100 automatic PFC unit
  • Integrated 100A MCCB for safe and reliable local isolation
  • Introduction of smaller capacitor stages to allow finer, more accurate correction

To future-proof the installation, the new unit was also specified with detuning reactors. These are essential in modern electrical environments where harmonic distortion is increasingly common, helping to protect capacitors and prevent resonance issues.

Installation & Commissioning

The work was carried out efficiently by a single PFC Engineering engineer, scheduled out of hours to minimise disruption to court operations.

The scope of works included:

  • Safe isolation and removal of the failed fuse switch and existing PFC equipment
  • Responsible disposal of all redundant components
  • Installation of the new FS100 PFC unit in the existing location
  • Installation of a new current transformer (CT) circuit for accurate system monitoring
  • Full testing and commissioning of the new system

The Result

The upgraded system now provides:

  • Accurate, stage-controlled power factor correction
  • Improved energy efficiency and reduced risk of penalties
  • Elimination of leading power factor during low-load periods
  • Enhanced safety with modern protection and isolation
  • Increased resilience against harmonic distortion

If your site is running an older or fixed PFC system, it may no longer be suitable for today’s dynamic electrical loads. PFC Engineering can carry out detailed inspections, load surveys, and upgrades to ensure your system is safe, compliant, and operating at peak efficiency.

Get in touch today to discuss your PFC requirements.

Central London Offices – PFC System Replacement

At PFC Engineering, we recently completed a comprehensive power factor correction (PFC) upgrade for a large office building in central London, replacing ageing components with a modern, high-performance solution.

Project Overview

The existing PFC system had reached the end of its service life, with original capacitors and 210Hz detuned reactors no longer providing reliable performance. To restore efficiency and ensure long-term stability, a full strip-out and rebuild was carried out. Prior to the repairs a load analysis determined that only half of the capacitors in each unit would be required to reach a healthy power factor of >0.95 inductive

Our Solution

Our engineers removed all the original capacitor banks and 210hZ reactors and installed a new system using high-quality components from Frako, including:

  • Frako 50kVar AM tray capacitor assemblies (480V rated)
  • 189Hz detuned reactors

This upgrade improves harmonic filtering, reduces system stress, and enhances overall power quality across the installation.

Delivery

The project was completed by a two-engineer team over a two-day period. Careful planning and on-site coordination ensured the works were delivered efficiently with minimal disruption to the building’s daily operations.

The Result

The upgraded PFC system now provides:

  • Improved power factor and energy efficiency
  • Increased reliability and lifespan of electrical infrastructure
  • A future-proofed solution aligned with modern load demands


Initial Findings

During a maintenance visit, the site’s existing power factor correction (PFC) equipment was found to be in a failed state. The following issues were identified:

  • 4 x 125 A DIN fuses had blown, leaving the system unprotected.
  • All 50 kVAr capacitor stages had failed, rendering the PFC system completely inoperative.
  • Given the age and condition of the equipment, an end-of-life replacement of all major components was strongly recommended.

For safety, the defective PFC unit was isolated and left offline, awaiting replacement works.

Replacement Works

A new modular PFC system was designed and installed as a like-for-like replacement for the original ABB equipment. The new trays were engineered to fit directly into the existing framework, allowing:

  • Reuse of existing power leads
  • Retention of original tray fixing points
  • Minimised installation downtime and site disruption

The replacement system incorporates several modern upgrades:

  • Soft-switching contactors – providing smoother capacitor engagement and reduced electrical stress.
  • 480 V rated capacitors – ensuring higher durability and better tolerance to supply variations.
  • Lovato DCRL5 fully digital controller – replacing the outdated relay with an advanced unit offering improved monitoring, automatic step adjustment, and greater accuracy in reactive power management.

Performance Outcome

Following installation, the PFC system successfully restored site efficiency. The gym’s power factor improved from 0.81 inductive to unity (1.00), eliminating excess reactive power demand and significantly reducing the risk of utility penalty charges.

The upgraded PFC not only restores compliance but also delivers:

  • Improved energy efficiency
  • Reduced strain on electrical distribution equipment
  • Extended lifespan of connected plant and machinery
  • A more stable and resilient electrical supply for the site’s daily operations


During a planned maintenance visit to the college’s LV distribution system, engineers discovered a complete failure of the existing power factor correction (PFC) equipment. All six 25 kVAr capacitor units had failed, and four 100 A DIN fuses were found to have blown. This failure left the site operating with no functional PFC, increasing the risk of higher reactive power charges and potential strain on the electrical infrastructure.

A detailed site load test was carried out to establish the actual reactive power requirements under normal operating conditions. The results confirmed that a total of 100 kVAr correction capacity would be more than sufficient to consistently maintain a site power factor above 0.96, comfortably within recommended efficiency standards.

To modernize and simplify the installation, the three failed ABB 25/25 kVAr modules were decommissioned and removed. These were replaced with a single 100 kVAr SBA tray, configured with four independently switched 25 kVAr soft-switching steps. This modular setup ensures greater flexibility, smoother operation, and reduced electrical stress compared to the original equipment.

In addition, the outdated reactive control relay was upgraded to a fully digital Lovato DCRL5 controller. This modern unit provides advanced monitoring, automatic step regulation, and improved accuracy in managing reactive power demand.

The upgrade not only restores reliable PFC capability but also improves system efficiency, reduces electrical losses, and minimizes the likelihood of future reactive energy penalties.


Following a review of the load at this large UK food manufacturer, it was found that the standard Power Factor Correction equipment was beginning to elevate low levels of background harmonics above 3% VTHD, causing premature failure of the capacitor banks. Due to space limitations, it was decided to remove all the existing standard PFC components and replace them with our fully detuned 189Hz PN54 Trays.


Each tray consists of 1 detuning reactor, a soft switching 415V contactor and a 50kVAr 480V rated capacitor bank. As well as the new tray assemblies, we also upgraded the control relay to the more reliable fully digital Lovato DCRL5 and installed additional forced air ventilation to help keep the reactors cool while under load.

With 2 units being rebuilt the same way, all works were carried out by a single engineer over 2 days without any disruption to the site’s load.


We were asked to carry out a service of a Power Factor Correction unit at a Brick Factory near Huntingdon, UK, that had no previous service history since its installation in 2011.

During our investigation, we found multiple failures of the internal components including failed capacitor banks, contactors that had welded themselves closed, multiple fuse failures and a high amount of dust and debris inside the cubicle.

Due to the high amount of failures, high levels of dirt and lack of annual servicing we recommend an end-of-life replacement of the PFC panel with a new FS300 Unit.

The new power factor unit would consist of 5 x 50kVAr capacitor stages and 2 x 25kVAr stages allowing for finer correction at lower loads. Incorporating high quality, long-life metallized polypropylene capacitors (480V rated) with over-pressure disconnection devices and discharge resistors fitted.

The unit would also include a built-in 630A load break switch and forced air ventilation.


Using the existing power and C.T cables the old unit was stripped down and removed from the site and the new FS300 was placed in the same position as before at the end of the LV panel. When in operation the unit would bring the site’s power factor up from 0.80 indictive to unity with 200kVAr of capacitors in circuit.


An end-of-life replacement was required for an old Power Factor Correction unit at a supermarket in central London.

A new wall-mountable FS100 PFC unit was to be installed using the existing power and C.T connections. The unit would incorporate 4  25kVAr capacitor banks, 480V rated with IMO MC32 soft switching contactors, sub fusing and additional forced air ventilation.


The unit would be controlled via a local Lovato DCRL 5 digital control relay and also include an integrated 200A load break switch for local isolation.


When operating the site power factor would be improved from 0.81 inductive to a unity power factor helping to save money on the monthly electricity bills by removing any reactive charges.


This unit was installed in 1 day by 1 engineer during normal working hours without any disruption to the site’s supply.


This 350kVAr Power Factor Correction unit installed in 1998 was found to have multiple capacitor failures following a long period of not being annually maintained.

It was decided that an end-of-life replacement for all the tray assemblies would be the best option. As such we swapped out the old-style SBA trays with its cascaded contactor steps with a more modern SBA tray with two 50kVAr soft switching contactors on each and 480V-rated capacitors.

We also included a smaller tray with two stages of 25kVAr for finer correction at different loads.

As well as this we also installed forced air ventilation into the front of the panel to help regulate the internal temperature of the unit.


We were asked to carry out a full maintenance of a panel built Power Factor Correction unit at a UK rubber fabrication plant.

The existing PFC on site had not had a full service before despite being installed in 1997. The unit has a multitude of component failures including the failure of capacitor banks, contactors that had welded closed, burnt-out inrush coils and operated fuses.

Due to the age of the equipment and the lack of annual servicing we recommended an end-of-life replacement to the panel and the installation of a new FSi200 fully detuned PFC unit.

The new unit would consist of 3 stages of 50kVar and 2 smaller stages of 25kVAr all controlled by an 8 stage Lovato DCRL 8 digital control relay. We would also include additional forced air ventilation and filtered louvres.

Due to the construction of the existing panel, we were able to remove the PFC section entirely and put the new unit in its place. New power cables were installed and connected to the existing MCCB that fed the old equipment.


All the works were carried out by 2 engineers during normal working hours without any disruption to the site supply.